Recent innovations in factory price large capacity refrigerated centrifuge technology focus on the improvement of automation as well as information integration. Intelligent models now communicate with laboratory information management systems so that the recording of experimental parameters is no longer problematic. Noise reduction modules and ergonomic covers have also increased user comfort and safety. Also, controlled temperature chambers and high-speed rotors facilitate the handling of sensitive material without degradation. Such technology renders factory price large capacity refrigerated centrifuge equipment more adaptable to varying research needs, offering unparalled precision in particle separation and purification processes in countless industries.

The applications of factory price large capacity refrigerated centrifuge span numerous scientific and industrial uses. In medicine, it is used to isolate blood components for transfusion and diagnostic purposes. In molecular biology, researchers use factory price large capacity refrigerated centrifuge to isolate DNA, RNA, and proteins for genetic studies. The pharmaceutical industry uses it to purify chemicals and enhance the quality of products. Environmental laboratories use factory price large capacity refrigerated centrifuge to test water and soil samples for contamination. Even in food processing, it aids in the cleansing of juices and the removal of oils. Its applicability ensures consistent outcomes in fields that require careful separation of substances.
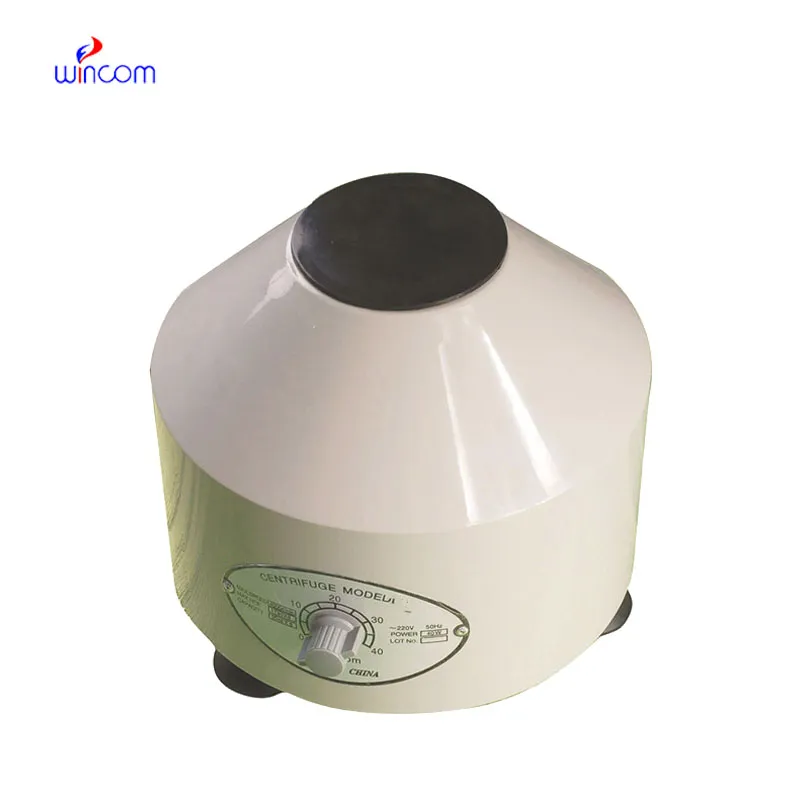
factory price large capacity refrigerated centrifuge will integrate digital intelligence and cutting-edge engineering in the years to come. Complex algorithms will auto-tune parameters for optimum efficiency and safety. Energy-optimized designs will keep operating costs at a minimum and help support global green efforts. Robotics integration will facilitate round-the-clock unattended operation in big production setups. Modular design will provide ease of customization, allowing users to set up factory price large capacity refrigerated centrifuge for specific scientific or industrial uses. These improvements will allow factory price large capacity refrigerated centrifuge to not only increase performance but also establish new standards for automation, accuracy, and sustainability in the lab environments of the future.
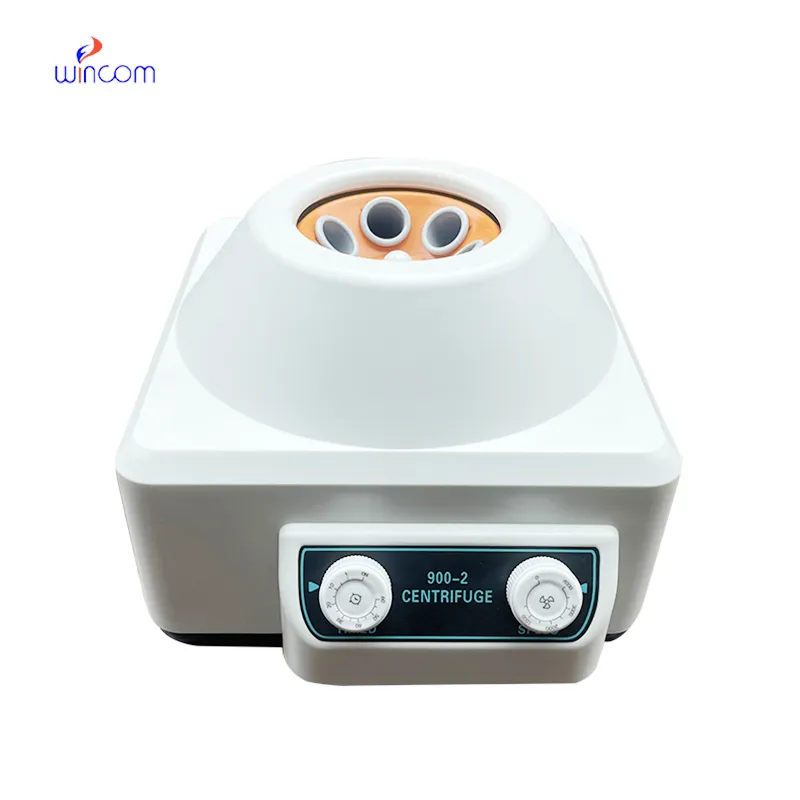
For long-term efficiency, factory price large capacity refrigerated centrifuge must be maintained with thorough attention to detail of operation. Every rotor and adapter must be checked for integrity before sample loading. After every cycle, the apparatus needs to be washed with neutral detergents and dried thoroughly. Vibration and mechanical stress are prevented by regular tests of balance. Seals and filters need to be replaced according to service schedules. Dust deposition is prevented by keeping the instrument in a covering when not used. If factory price large capacity refrigerated centrifuge apparatus is cared for according to disciplined procedure, equipment will give consistent high-performance performance year in year out.
A factory price large capacity refrigerated centrifuge is a universal gadget designed to separate parts in a mixture through sheer spinning power. A factory price large capacity refrigerated centrifuge operates through the principle of sedimentation, in which heavier particles move outwards and lighter particles remain at the center. Employed within laboratories, clinics, and industry in general, a factory price large capacity refrigerated centrifuge may be utilized to separate materials such as blood plasma, proteins, and chemical reagents with accuracy. Modern factory price large capacity refrigerated centrifuge exist in various forms, from benchtop to industrial types and ultracentrifuges, all for specialized applications. They are accurate and reproducible, a necessity in production and research.
Q: What is a centrifuge used for? A: A centrifuge is used to separate mixtures based on density differences by spinning them at high speeds, allowing heavier particles to settle away from lighter ones. Q: How does a centrifuge work? A: A centrifuge operates by generating centrifugal force, pushing denser materials outward while lighter components remain near the center, resulting in effective separation. Q: What are common applications of a centrifuge? A: Centrifuges are used in laboratories, hospitals, and industries for blood testing, chemical analysis, purification, and sample preparation. Q: How often should a centrifuge be calibrated? A: Calibration should be performed at least once a year or whenever performance inconsistencies appear to ensure accuracy and reliability. Q: Can a centrifuge handle biological samples? A: Yes, many centrifuges are designed for biological materials such as blood, plasma, and cell cultures under controlled and sterile conditions.
The microscope delivers incredibly sharp images and precise focusing. It’s perfect for both professional lab work and educational use.
The centrifuge operates quietly and efficiently. It’s compact but surprisingly powerful, making it perfect for daily lab use.
To protect the privacy of our buyers, only public service email domains like Gmail, Yahoo, and MSN will be displayed. Additionally, only a limited portion of the inquiry content will be shown.
Hello, I’m interested in your centrifuge models for laboratory use. Could you please send me more ...
Hello, I’m interested in your water bath for laboratory applications. Can you confirm the temperat...
E-mail: [email protected]
Tel: +86-731-84176622
+86-731-84136655
Address: Rm.1507,Xinsancheng Plaza. No.58, Renmin Road(E),Changsha,Hunan,China


 EN
 af
 es
 ar
 tr
 sw
 pt
 th
 ur
 bn
 ne
 vi
 km
 lo
 de
 ru
 fi
 nl
 fa
 fr
 ko